Incomplete joint penetration: what it is and how to spot it
Incomplete joint penetration is a groove weld whose metal stops short of the depth the joint design calls for. In a joint meant to be welded through, the root faces are left unmelted, often with a gap between them. It can be open to the back of a single-sided weld or hidden in the middle of a double-sided one.
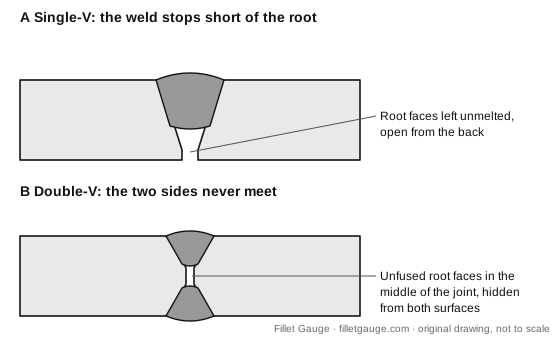
Use this diagram
How to recognize incomplete joint penetration
- Look at the back first. On a single-sided complete joint penetration weld, the root side should show a fused bead. If you can still see the square edges of the root faces, or a gap between them, the weld didn't get through.
- Check the design. Not every groove weld is meant to go through. A partial joint penetration groove weld is designed to stop at a set depth. Read the welding symbol and the drawing before you call it a discontinuity.
- Read the film. On a radiograph, unmelted root faces with a gap show as a straight, sharp-edged dark line along the center of the root. The straightness comes from the machined edges.
- Feel for it in a section. A macro of a double-V joint with incomplete penetration shows a thin unfused band across the middle where the two welds failed to meet.
Try one question
Question 1 of the free 10-question check on CWI Part B. No signup. Then ask Tack, the AI study buddy, why the answer is right and the others are wrong.
NDE Application
A conventional radiograph of a steel groove weld shows a straight, sharp-edged dark line running along the center of the root for about 2 in. What is the most likely discontinuity?
Press A–D or 1–4 to choose an answer while this question is on screen.
Choose an answer to begin
How it is measured
Where the back is accessible, visual inspection finds it directly, and a mirror or borescope helps on pipe. You record its length along the weld and, when a document asks, how much of the root is unfused. Where the back isn't accessible, radiography or ultrasonic testing does the work. Always compare against the governing document for that joint type, since a weld designed as partial penetration has a different requirement altogether.
Ask Tack before you buy AI your Fillet Gauge study buddy
See what's on the CWI Part B exam, test yourself with 5 quick questions, or find the plan that fits you.
The CWI Part B course
Available now · instant accessLearn the tool kit, the specification and the qualification records, then practice.
- 7modules of lessonsEvery task on the outline
- 3full-length timed exams46 questions in 120 minutes each
- 338practice questionsEach one explained
- 2worked calculationsStep by step
- 21specification drillsFind it fast in the Book of Specifications
- 1week-by-week study planSet to your exam date
Turn a practice answer into a study step. In untimed practice, ask Tack AI about any question you answer, follow up, then see your weakest topics and what to drill next.
Instant access. Terms and refunds · Secure checkout by Stripe · Billed by Nori Software
- Parts B + C bundle$169$29 less than buying both courses separatelyIncludes the CWI Part B and CWI Part C D1.1 courses
Terms and refunds · Secure checkout by Stripe · Billed by Nori Software
- Full CWI prep$249$48 less than buying the 3 courses separatelyIncludes the CWI Part A, CWI Part B and CWI Part C D1.1 courses
Terms and refunds · Secure checkout by Stripe · Billed by Nori Software
- Free sample lessonFree
- Question of the dayFree
Every answer comes with a full explanation.
Common mix-ups
- Incomplete penetration or incomplete fusion. Penetration is about depth: did the weld reach the root? Fusion is about bonding to a surface higher up. A fully fused root rules out incomplete penetration.
- Incomplete penetration or root concavity. With root concavity the root did melt through but the back surface sits dished in. With incomplete penetration the root faces were never melted.
- Incomplete penetration or a root crack. A crack is jagged with pointed ends. The dark line from unmelted root faces is straight and even.
Why it forms
The root opening is too tight or the root face too thick for the heat being used. The current is too low, the travel too fast, or the electrode too large to reach into the root. Misalignment between the members can leave one root face out of reach. On double-sided welds, poor back gouging leaves unmelted metal from the first side.
Incomplete joint penetration on the CWI exam
On Part B, it belongs to Welding Inspection and Discontinuities, at least 34% of the practical, and shows up in NDE Application when a radiograph or report is involved. On Part A it fits Visual Examination, NDE Fundamentals and Symbols, where you read whether a groove weld is meant to go through. On Part C, find the code's requirement for complete joint penetration welds in your own copy.
Practice it
Separate it from its look-alikes in the weld discontinuities quiz. Then read its sidewall partner, incomplete fusion, and its opposite at the root, burn-through. All types are in the weld discontinuities guide.
Check the rest of Part B
Take the free 10-question check. It's weighted to the Part B outline, scored by domain and needs no signup, so you see your Part B weak spots before you plan your study weeks.
Sources
Show the list
- Weld Defects / Imperfections: Incomplete Root Fusion or Penetration (Job Knowledge 40), TWI. Retrieved 25 Oct 2026.
- CWI Part B Practical Examination Information, American Welding Society, Rev. 03.01.2024. Retrieved 20 Oct 2026.
- Discontinuity names follow AWS A3.0, Standard Welding Terms and Definitions. Every description here is our own wording.
Facts checked 25 October 2026 against the sources listed above. If something has changed, tell us and we will correct it within 2 business days.
Your next step
Ready to see where you stand on CWI Part B?
Free, untimed and scored by domain. No signup.
Start the free 10-question checkPart B course. Lessons, timed practice exams and a plan around your exam date. Get Part B course · $99 See the plans or read the free sample lesson.Terms and refunds
Want a timed run? Try the free 25-question mini-mock. The first 5 need no email.
Prefer paper? Free printables
- Print a class quiz (free PDF). 5 practice questions with an answer key on page 2.
- Print the flashcards as cut-out cards (free PDF). The free flashcard sample, ready to cut and carry.
From the blog
- CWI Part B practice questions: drill measurements
- Visual weld inspection: before, during and after
- CWI Part B replicas and how to practice