Slag inclusion: what it is and how to spot it
A slag inclusion is nonmetallic solid, usually flux residue, trapped inside a weld or between the weld and the base metal. It forms with flux-shielded processes such as SMAW, FCAW and SAW when slag from one pass isn't removed before the next goes on, or when the arc can't melt it out of a notch.
Use this diagram
How to recognize a slag inclusion
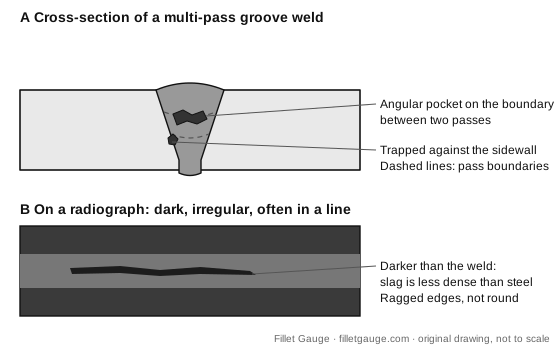
- Check the shape. Slag is irregular: angular corners, ragged edges, sometimes a long stringer. It is never the neat round void that gas leaves.
- Check where it sits. Slag collects where cleaning is hard. The usual spots are pass boundaries, the toe of an earlier bead where it meets the sidewall, and deep valleys between two beads laid side by side.
- Check the process. No flux, little chance of slag. A GTAW root is unlikely to hold slag; an SMAW fill pass may.
- Read the film. On a radiograph, slag is less dense than steel, so it shows darker than the weld, with ragged outlines. Long lines of it parallel to the weld are often called wagon tracks when they run along both toes of a root bead.
Try one question
Question 1 of the free 10-question check on CWI Part B. No signup. Then ask Tack, the AI study buddy, why the answer is right and the others are wrong.
Welding Inspection and Discontinuities
A convex fillet weld replica is checked with a leaf-type fillet gauge. The drawing calls for a single fillet size. The vertical leg fits the 3/8 in blade and the horizontal leg the 5/16 in blade. What size is recorded?
Press A–D or 1–4 to choose an answer while this question is on screen.
Choose an answer to begin
How it is found and sized
Most slag is buried, so visual inspection only catches it when it breaks the surface, for example at the face of a bead that wasn't cleaned before a cap pass. Radiography is the usual way to find it in a finished groove weld, and ultrasonic testing picks up larger inclusions. On a cut section or macro etch, slag looks like a dark, crumbly pocket. Where the governing document limits slag, it usually works on length, width or the spacing of inclusions, so record those carefully and look the limit up in that document.
Ask Tack before you buy AI your Fillet Gauge study buddy
See what's on the CWI Part B exam, test yourself with 5 quick questions, or find the plan that fits you.
The CWI Part B course
Available now · instant accessLearn the tool kit, the specification and the qualification records, then practice.
- 7modules of lessonsEvery task on the outline
- 3full-length timed exams46 questions in 120 minutes each
- 338practice questionsEach one explained
- 2worked calculationsStep by step
- 21specification drillsFind it fast in the Book of Specifications
- 1week-by-week study planSet to your exam date
Turn a practice answer into a study step. In untimed practice, ask Tack AI about any question you answer, follow up, then see your weakest topics and what to drill next.
Instant access. Terms and refunds · Secure checkout by Stripe · Billed by Nori Software
- Parts B + C bundle$169$29 less than buying both courses separatelyIncludes the CWI Part B and CWI Part C D1.1 courses
Terms and refunds · Secure checkout by Stripe · Billed by Nori Software
- Full CWI prep$249$48 less than buying the 3 courses separatelyIncludes the CWI Part A, CWI Part B and CWI Part C D1.1 courses
Terms and refunds · Secure checkout by Stripe · Billed by Nori Software
- Free sample lessonFree
- Question of the dayFree
Every answer comes with a full explanation.
Common mix-ups
- Slag or porosity. Round and smooth is gas. Angular and ragged is slag. Location helps too: porosity can be anywhere, slag likes pass boundaries.
- Slag or incomplete fusion. Both can sit on a sidewall. Incomplete fusion is a thin, even line that follows the groove face. Slag is a chunkier pocket of solid material.
- Slag or a tungsten inclusion. On film, slag reads dark and tungsten reads bright.
Why it forms
Poor interpass cleaning is the big one. Others are a convex bead that leaves sharp notches at its toes, an electrode angle that pushes slag ahead of the pool, too low a current to float slag to the surface, and a groove too narrow to reach. Undercut on the sidewall of an earlier pass makes a ready trap for the next layer's slag.
Slag on the CWI exam
On Part B, slag belongs to Welding Inspection and Discontinuities, at least 34% of the practical, and turns up again under NDE Application when you read a radiograph or a report. On Part A, it fits Visual Examination, NDE Fundamentals and Welding Application and Control, where cleaning practice lives. On Part C you look up how your code treats it in the NDT acceptance criteria.
Practice it
Test your read of radiograph images on the NDE methods quiz. Then compare slag with its round cousin, weld porosity, and with the flat flaw it hides beside, incomplete fusion. The weld discontinuities guide puts every type side by side.
Check the rest of Part B
Take the free 10-question check. It's weighted to the Part B outline, scored by domain and needs no signup, so you see where slag, porosity and the rest stand against your other domains.
Sources
Show the list
- Defects / Imperfections in Welds: Slag Inclusions (Job Knowledge 43), TWI. Retrieved 25 Oct 2026.
- CWI Part B Practical Examination Information, American Welding Society, Rev. 03.01.2024. Retrieved 20 Oct 2026.
- Discontinuity names follow AWS A3.0, Standard Welding Terms and Definitions. Every description here is our own wording.
Facts checked 25 October 2026 against the sources listed above. If something has changed, tell us and we will correct it within 2 business days.
Your next step
Ready to see where you stand on CWI Part B?
Free, untimed and scored by domain. No signup.
Start the free 10-question checkPart B course. Lessons, timed practice exams and a plan around your exam date. Get Part B course · $99 See the plans or read the free sample lesson.Terms and refunds
Want a timed run? Try the free 25-question mini-mock. The first 5 need no email.
Prefer paper? Free printables
- Print a class quiz (free PDF). 5 practice questions with an answer key on page 2.
- Print the flashcards as cut-out cards (free PDF). The free flashcard sample, ready to cut and carry.
From the blog
- CWI Part B replicas and how to practice
- CWI vs CAWI vs SCWI: the three AWS inspector levels
- Visual weld inspection: before, during and after